Project Overview
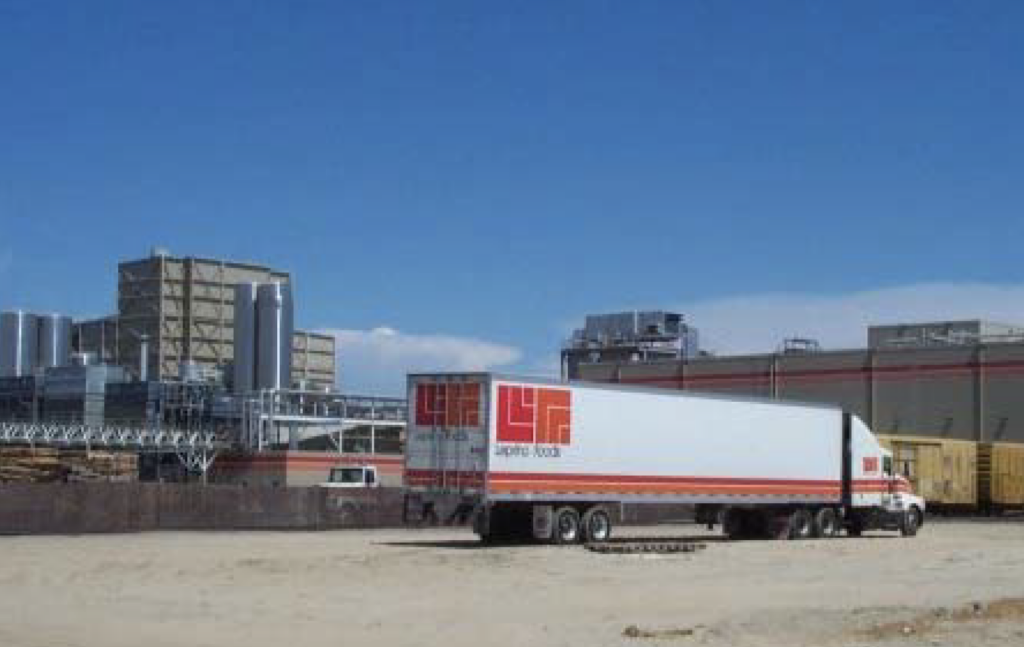
Customer: Leprino Foods
Location: Lemoore, California
Application: Selective Catalytic Reduction
The Challenge
Leprino Foods, a leading manufacturer of premium cheese and one of the largest U.S. exporters of whey products, was planning a major expansion of its Lemoore, California, facility. The expansion would create a 500,000- square foot cheese making and whey-processing operation and require additional steam capacity to support increased production.
In addition to meeting the facility’s growing steam demands, the new boiler system needed to comply with stringent Ultra-Low NOx requirements established by the San Joaquin Valley Air Pollution Control District.
The challenge was clear: increase steam capacity while controlling NOx emissions and improving overall plant efficiency.
The EcoCAT Solution
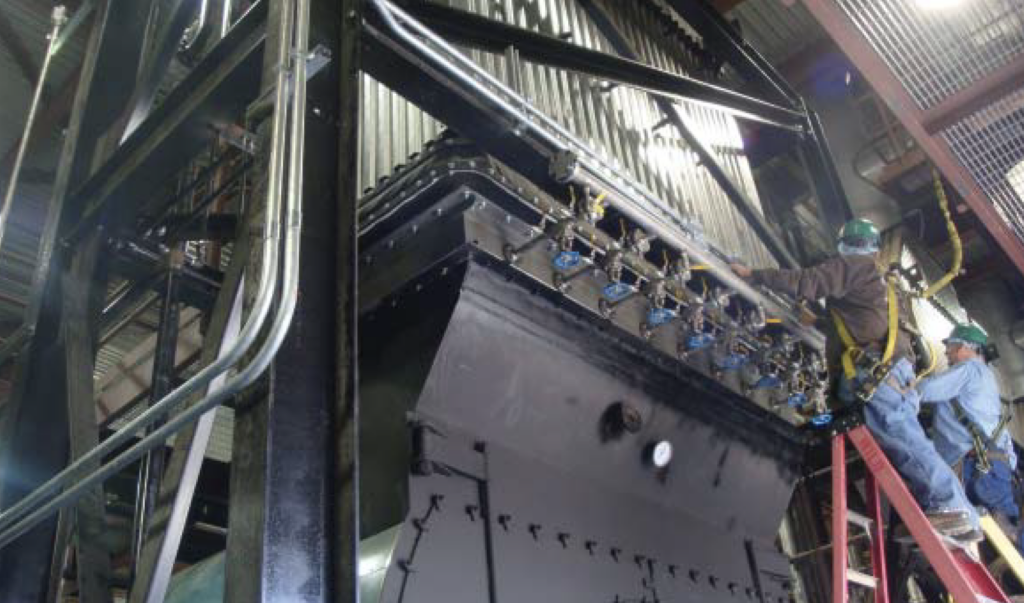
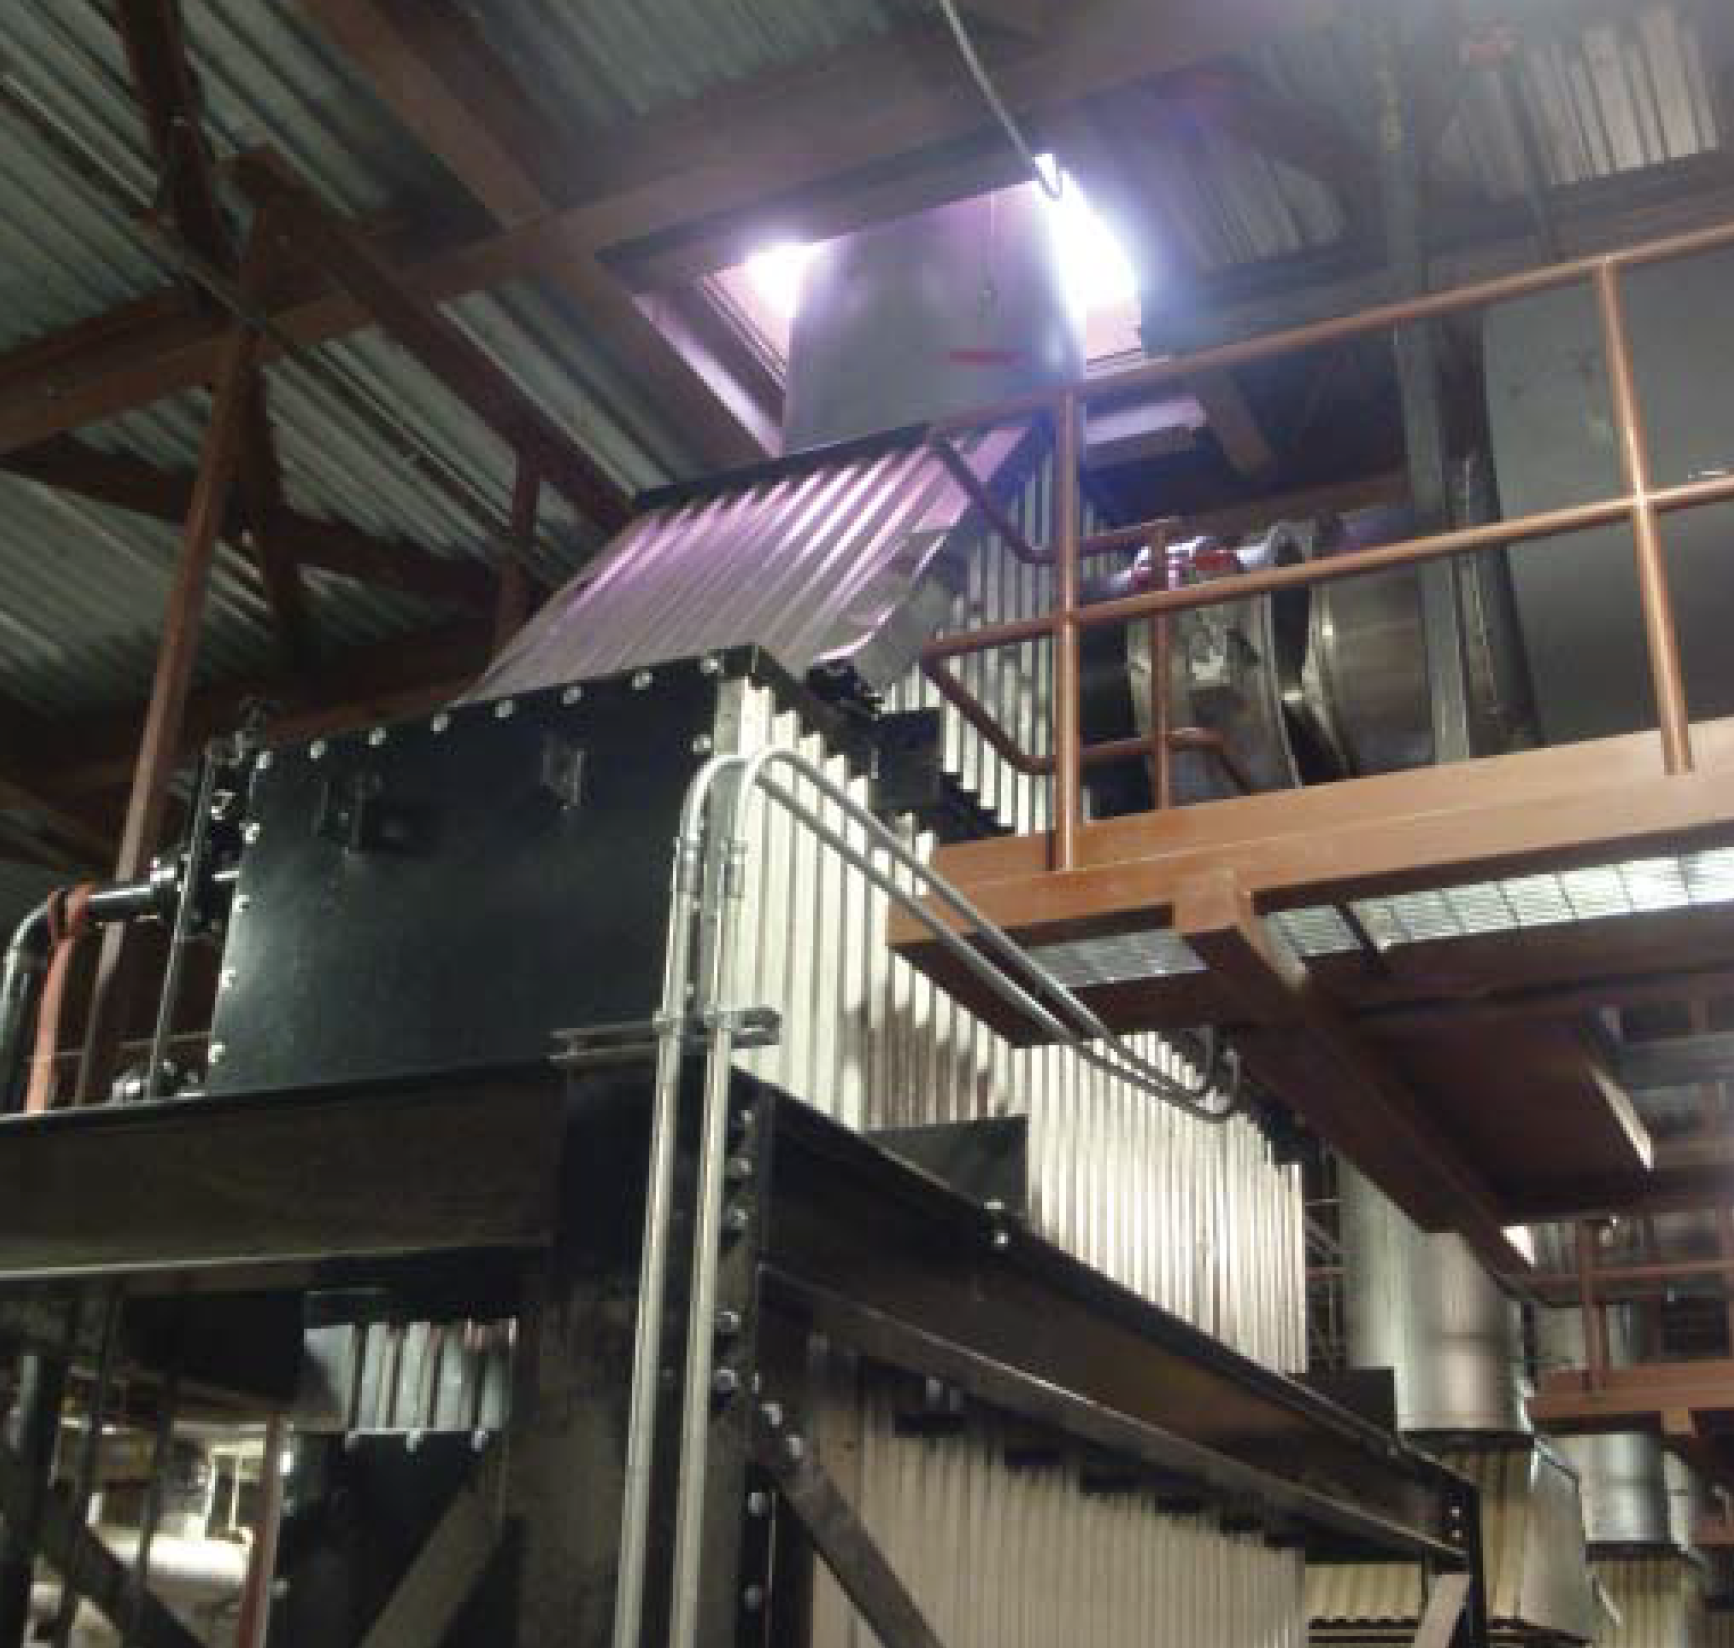
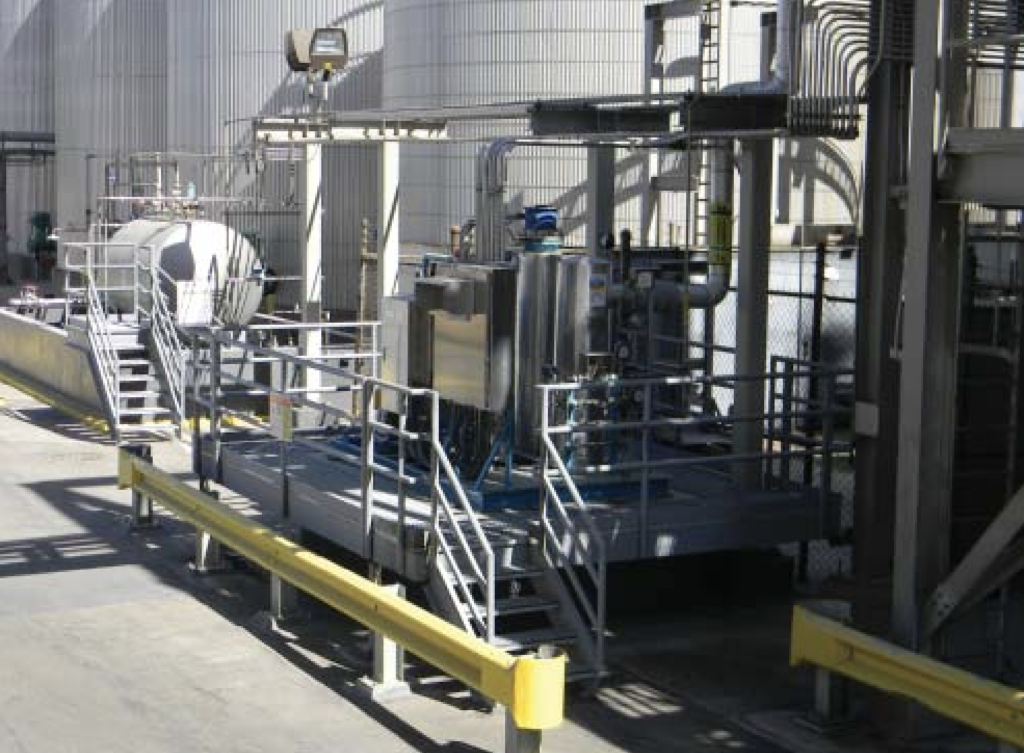
To support the facility expansion, a new 1.200 HP boiler system incorporating Selective Calalytic Reduction (SCR) was installed to meet the required Ultra-Low NOx emissions standards.
The complete boiler plant solution included:
- 1,200 HP Cleaver-Brooks Boiler
- Ultra-Low NOx SCR system
- Custom boiler controls and burner
- Condensing stack economizer
- Variable frequency drive (VFD) for the blower motor
- Condensate return system improvements
The SCR system provided the emissions-control technology needed to reduce NOx while allowing the facility to add the steam capacity required for its expanded production operations.
Efficiency Beyond Emissions Reduction
Emissions compliance was only one part of the project.
A condensing stack economizer and variable frequency drive were incorporated into the boiler system to improve energy efficiency. Improvements were also made to the condensate return system to enhance deaerator operation and maximize condensate recovery.
Together, these improvements helped reduce fuel and water consumption while supporting the facility’s overall environmental and operational goals.
The Result
The completed boiler and SCR installation provided Leprino Foods with the additional steam capacity needed to support its expanded Lemoore production facility while meeting applicable Ultra-Low NOx requirements.
By integrating SCR emissions control with boiler plant efficiency improvements, the facility was able to address three critical objectives within one project.:
Increased Steam Capacity | Ultra-Low NOx Compliance | Improved Efficiency
For industrial facilities facing increasingly stringent NOx requirements, EcoCAT SCR systems provide a proven approach to emissions reduction without sacrificing the steam capacity and performance required for production.
Need to reduce NOx emissions from an existing HRSG or industrial process? Contact EcoCAT to discuss an SCR solution engineered for your application.
Contact our emissions specialists to discuss your SCR application.